Monitoring Transport Flow in Meat Processing Plants
18GF Series Thru-Beam Sensor Operates Reliably in Fog and Extreme Environments
The Application
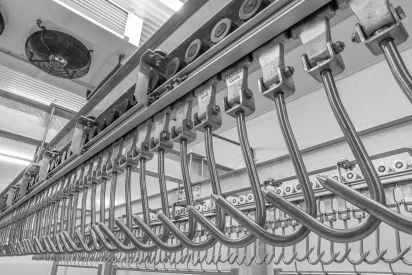
In meat processing plants, the transport flow of meat in refrigerators and processing lines must be monitored and controlled. The proposed sensor solution must be highly reliable and operate effectively and without false detections despite the challenging conditions of the environment. This includes withstanding a foggy environment following hot water cleaning processes, which include significant temperature fluctuations from -10 º C to +50 º C. A rugged, well-built, high-performance sensor is critical to maintain accurate operation in these extreme conditions and ensure uninterrupted and precise control of the meat handling process.
The Goal
The biggest challenge in this application is operating in a foggy environment, typical of industrial meat processing plants, where the sensors must be built strong enough to operate reliably. The sensors must accurately detect the presence of meat while ignoring interference caused by the fog. To address this, the devices require a housing that ensures both durability and reliability. Specifically, the sensors must meet IP68 degree of protection, providing resistance against the ingress of water. This level of protection is crucial to withstand the harsh conditions in these processing plants and ensure consistent and accurate operation.

The Solution
The previous solution was a thru-beam sensor with IP68 degree of protection, however due to the drastic temperature fluctuations during cleaning, the sensor lens was condensed during the process. The 18GF series photoelectric thru-beam sensor proved to be the ideal solution for the application after testing and evaluating various IP68-rated products. This high degree of protection ensures longevity and reliability due to its fully sealed housing, allowing it to withstand harsh conditions such as moisture, fog, and extreme temperature fluctuations. The lens of the 18GF sensor (70169398 OBE10M-18GF60-S2PP-0,3M-V1-IR) has been specifically designed to prevent condensation, assuring continuous and accurate detection of meat during transportation.
Technical Features
- Sensing range 10 m
- With increased sealing, degree of protection (IP68)
- Narrow opening angle, reduces mutual interference between pairs
- Not sensitive to ambient light
- Short-circuit protected
- M18 threaded housing design

The Benefits
By using our device, the customer can benefit from sturdy sensors that are designed for reliable performance in extreme temperature fluctuations (-10 ºC to +50 º C) and can withstand demanding environments and cleaning processes. The device ensures accurate detection even in demanding environments, such as fog, while maintaining high performance and control over the production process. Our commercial and technical support teams are readily available to address any inquiries and minimize potential concerns, further ensuring customer confidence and satisfaction.